Classification Framework
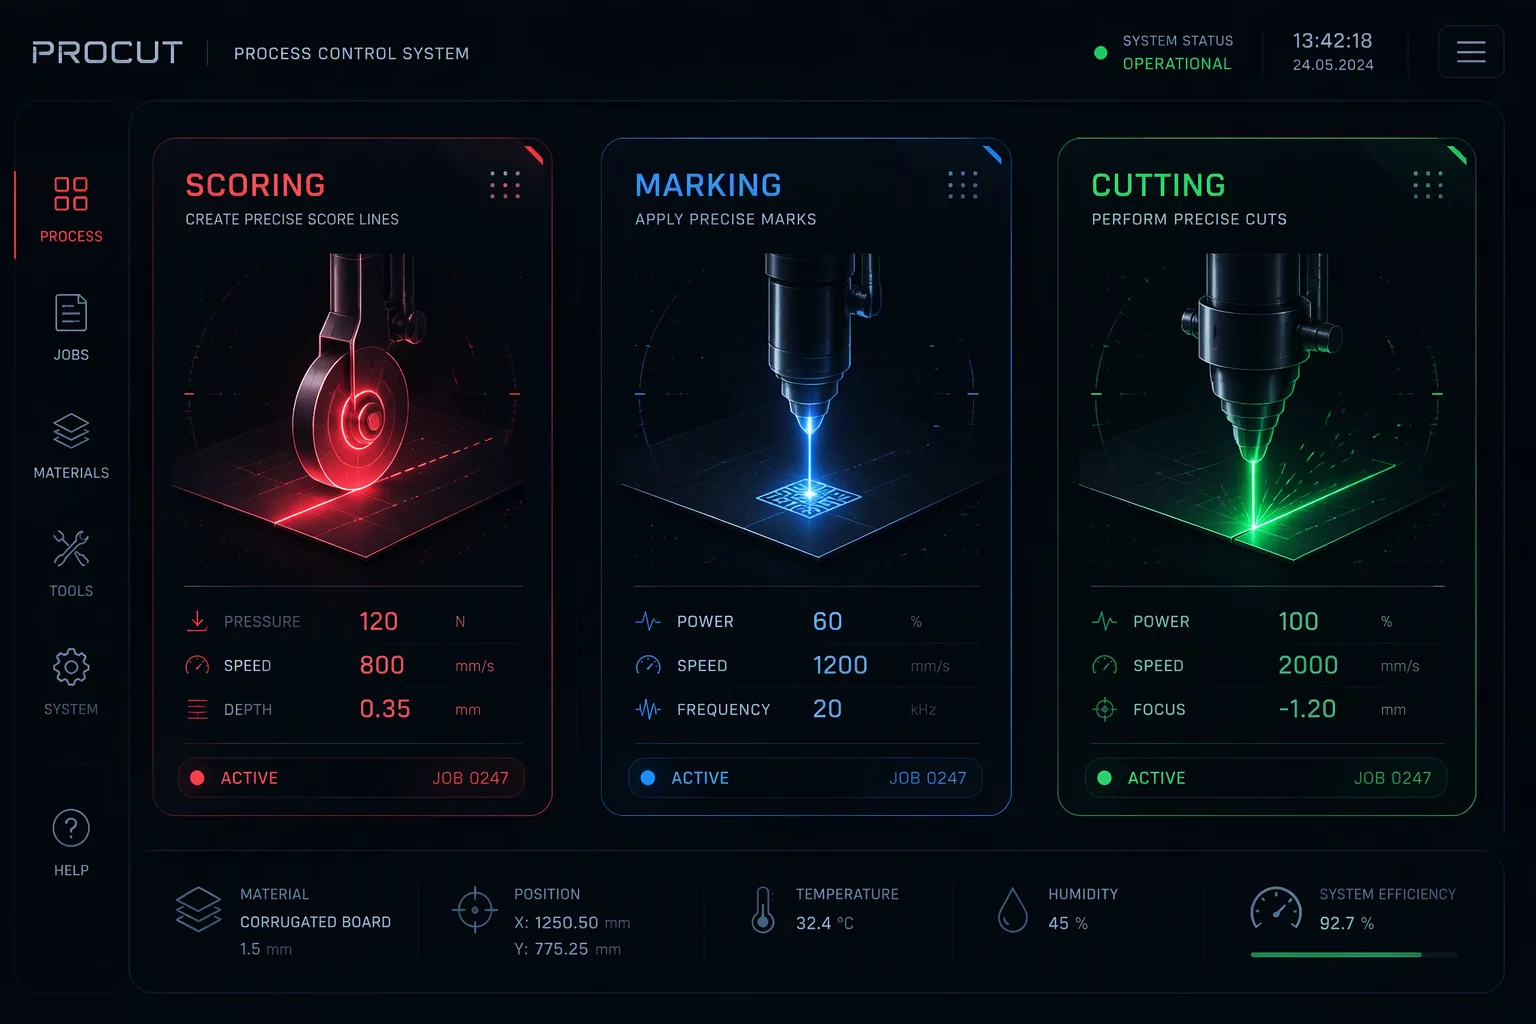
Every laser manufacturing file relies on three foundational process types: raster fills for dark surface rendering, high-speed vector lines for marking, and penetrating through-cuts for physical separation. Assigning each graphic entity to its true functional category prevents unexpected burn-through, thermal warping, and lost mechanical registration during execution.
When design files arrive with overlapping geometries, operators frequently confuse high-speed vector scoring with perimeter cutting. Isolating these processes into designated software layers is intended to help that air pressure, power curves, and travel velocities adapt automatically to the intended depth of each stroke.
Laser Energy Application
The mechanical behavior of your CNC gantry dictates the ideal sequence for these operations. High-speed bidirectional scanning must always precede slow, high-power through-cuts to maintain complete workpiece immobility throughout the job.
- Raster Engrave (Fill): Executes high-speed horizontal sweeping with low air assist to ablate surface material without displacing the target stock.
- Vector Score (Line Mark): Applies continuous low-power beam tracking along vector paths to score folding creases and aesthetic hair lines.
- Through-Cut (Full Separation): Employs high power, reduced feed rate, and maximum air assist to sever components cleanly from the parent sheet.
Executing a through-cut prematurely drops the part onto honeycomb supports or tilts it slightly off-axis. Subsequent raster passes over a tilted part will suffer from severe focal blur, uneven charring, and permanent dimensional distortion.
Material Stability Rules
Before sending the compiled g-code to the machine controller, inspect the layer stack in the preview simulator. Confirm that all raster passes reside at the top of the stack, vector scores sit in intermediate positions, and internal hole cuts precede final perimeter cutouts. This disciplined order safeguards delicate geometries and eliminates ruined stock.